Cooling and Heating in Balance
Industrial NH₃ refrigeration, heat recovery and precise process control for a sustainable beverage production facility
A modern beverage production facility requires large amounts of both cooling and heating. Products need to be cooled, while various production and cleaning processes require heat. By intelligently combining these processes, significant opportunities arise to improve energy efficiency.
For a new, sustainable production facility operated by an international beverage manufacturer, an innovative energy concept was developed in which industrial ammonia refrigeration and heat pumps work closely together. In this industrial-scale 'blender', available energy is recovered and reused wherever possible.
Wijbenga supported the refrigeration contractor with technical engineering, component selection and the supply of key components for the installation. A large-scale project in which fully welded Vahterus heat exchangers and a substantial number of pneumatically actuated RTK control valves play an important role.
The challenge: generating cooling while making optimal use of heat
In the food and beverage industry, refrigeration and heating are closely interconnected. Traditionally, a significant proportion of the heat generated by industrial refrigeration systems is rejected to the environment.
For this production facility, an integrated energy concept was selected. The refrigeration system and industrial heat pumps work together to provide heat at different temperature levels. Large volumes of water are heated to 65 °C and 90 °C for use in various production processes.
This combination requires high-quality heat exchangers and precise control of ammonia flows under widely varying operating conditions.
 The solution: reliable heat transfer with Vahterus
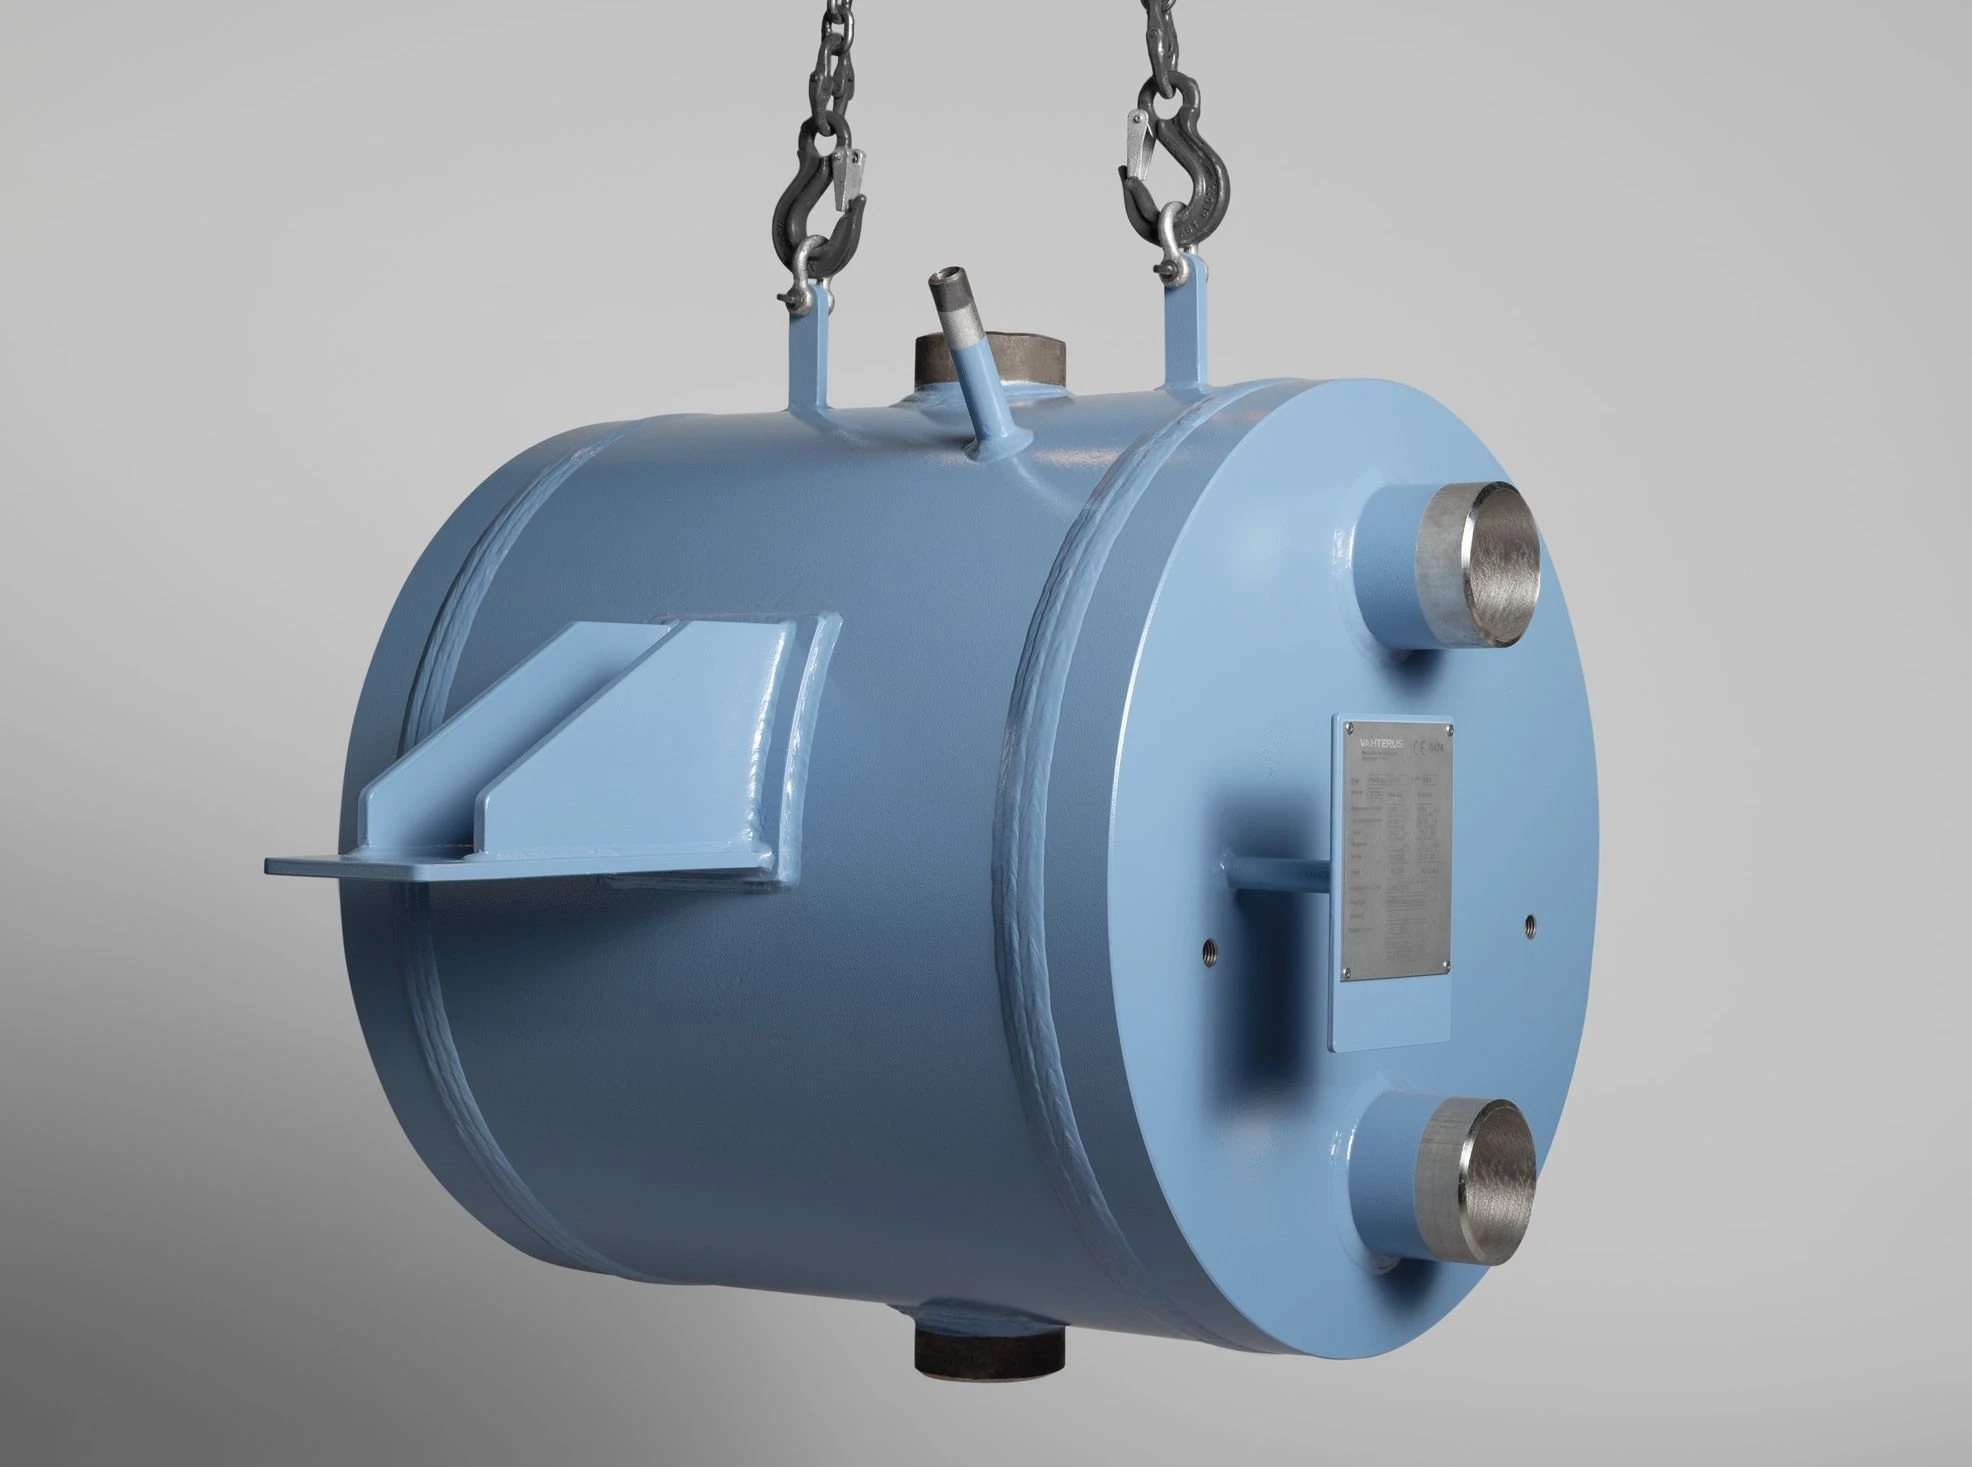
For the various refrigeration and heat pump circuits, Wijbenga supplied a series of fully welded Vahterus Plate & Shell heat exchangers. The scope of supply included desuperheaters, condensers and subcoolers, selected to meet the specific temperature and pressure requirements of the installation.
Particular attention was paid to operational reliability and water quality when selecting the materials. Several heat exchangers feature plates manufactured from high-grade 254SMO stainless steel, which offers enhanced resistance to chloride-containing media and stress corrosion cracking.
The fully welded construction, without gaskets between the media, contributes to reliable heat transfer. This is an important feature for installations where operational reliability and production continuity are essential.
Precise NH₃ control with RTK
A particularly notable aspect of this project is the extensive supply of industrial control valves from RTK Regeltechnik Kornwestheim.
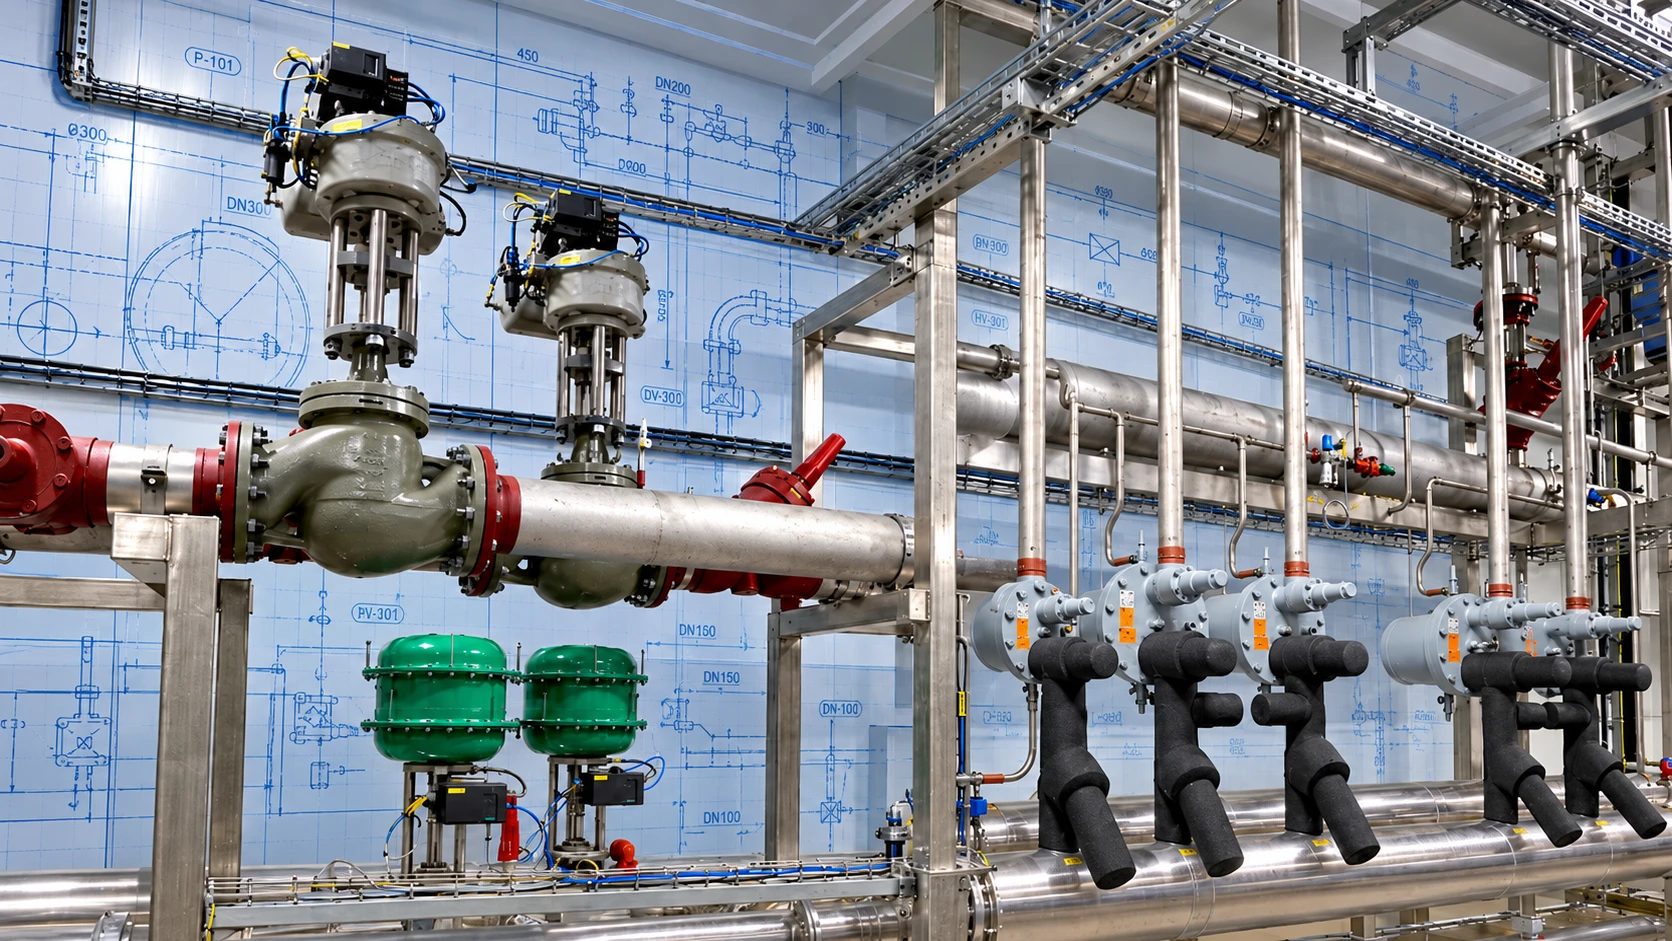
To control the ammonia flows at different pressure and temperature levels, Wijbenga supplied dozens of control valves, including expansion valves, hot-gas control valves and suction-gas control valves.
Many of these valves are equipped with pneumatic actuators and electronic valve positioners. This allows ammonia flows to be regulated accurately and consistently, according to the actual operating conditions.
The combination of carefully selected valve characteristics, reliable pneumatic actuators and precise valve positioning is essential for stable system operation. Particularly when different refrigeration and heat pump circuits operate together, accurate control provides the foundation for efficient and reliable performance.
 Wijbenga's contribution: technical support and component selection
In an installation of this scale, selecting heat exchangers and control valves involves much more than simply determining the required capacity or connection size.
Wijbenga was closely involved in the technical engineering and selection of the supplied components. Different operating conditions, pressure differentials, material requirements and control characteristics had to be carefully evaluated and matched.
Through close cooperation with the refrigeration contractor and manufacturers Vahterus and RTK, suitable solutions were selected for the various parts of the refrigeration system.
A sustainable solution with lasting value
This production facility demonstrates how industrial refrigeration and heat generation can be integrated into a single, efficient energy concept.
By recovering and reusing available heat and precisely controlling ammonia flows, the system provides a solid foundation for energy-efficient and reliable operation.
Even years after its completion, this project remains an impressive reference for Wijbenga. It demonstrates how technical expertise, high-quality components and close cooperation contribute to future-proof industrial refrigeration and heat pump systems.
Efficient heat transfer. Precise control. Reliable technology.